Grade Designations.
| BS EN 10083-3 | 36CrNiMo16 / 1.6773 |
| BS 970:1991 (withdrawn) | 835M30 |
| BS 970:1955 | EN30B |
| Also referenced as | 30CrNiMo16-6 / 1.6747 |
| Material class | ~4% Ni-Cr-Mo through hardening |
Grade-equivalence naming varies by supplier and is conventional rather than an exact chemistry match — confirm against your EN 10204 certificate where precise cross-referencing matters.
Availability & Supply Condition.
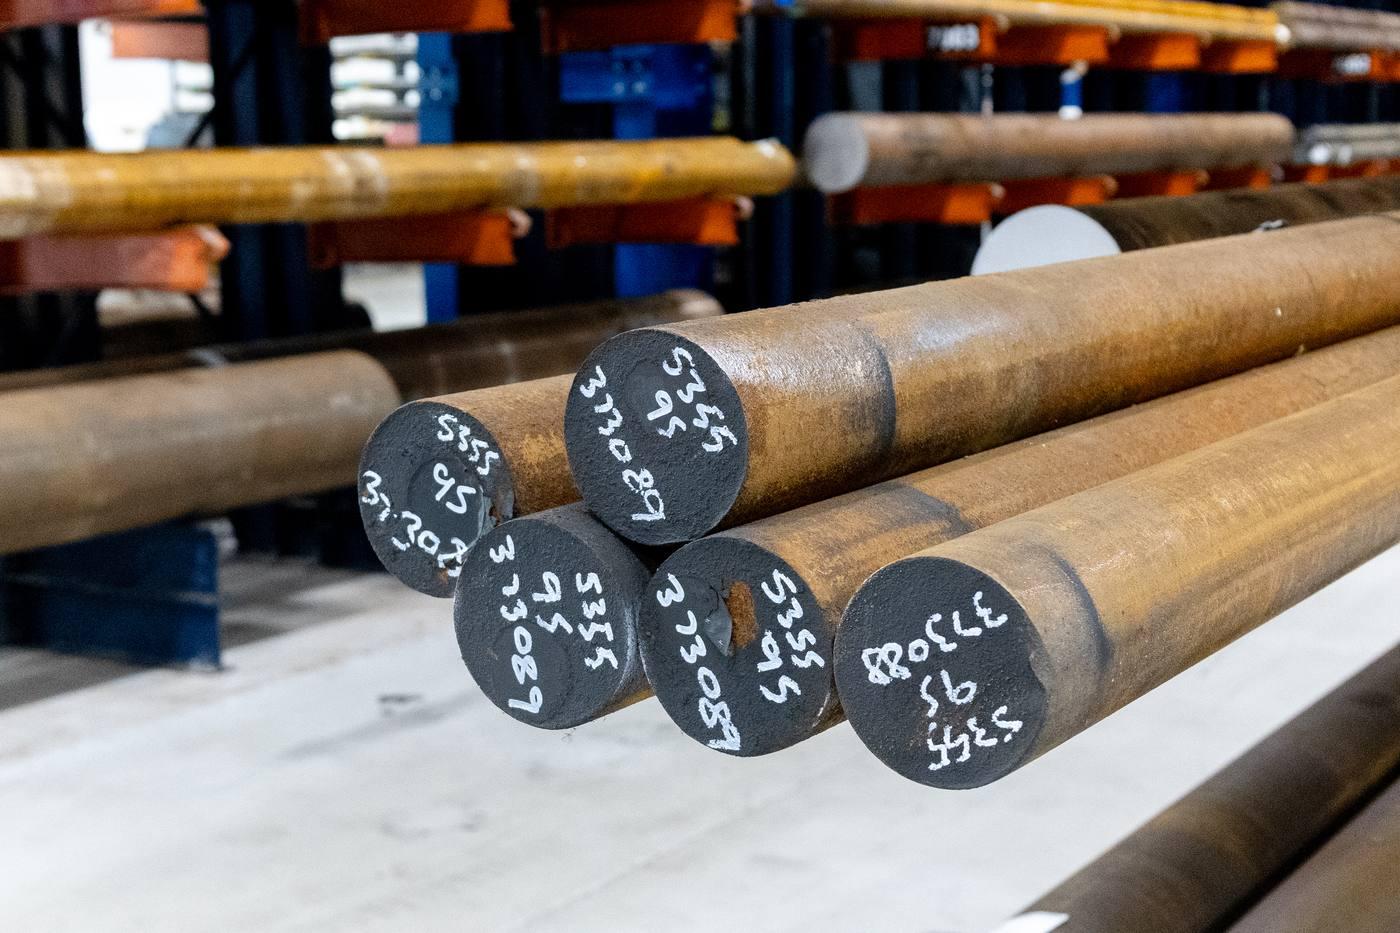
Black Rounds: 40–300mm
Supply condition: Hot Rolled Black, typically supplied as rolled or annealed (285 HB max annealed). Black bar only — this grade is not stocked as bright bar.
Cut to length from 1 piece — −0/+2mm standard tolerance — 2–3 day turnaround — Cutting service details ›
Chemical Analysis.
Values shown as percentages by weight (% wt). Values are ranges unless stated as maxima.
| Designation | C | Si | Mn | P max | S max | Cr | Ni | Mo |
|---|---|---|---|---|---|---|---|---|
| 835M30 | 0.26–0.34 | 0.10–0.35 | 0.40–0.60 | 0.050 | 0.050 | 1.10–1.40 | 3.90–4.30 | 0.20–0.40 |
For full chemical analysis with heat number, request an EN 10204 3.1 material test certificate when ordering — available on all alloy grades. Certificate types explained ›
Each alloying element does a specific job: the ~4% nickel gives toughness and shock resistance; chromium adds hardenability and wear resistance; molybdenum carries hardenability deeper into large sections and resists temper brittleness. Together they are what allow this grade to harden fully on air cooling alone.
Mechanical Properties.
Values shown for standard supply condition and after hardening and tempering. Properties vary by section size and heat treatment condition.
| Condition | Tensile Rm (N/mm²) | Yield Re (N/mm²) | Elongation A% | Hardness HB |
|---|---|---|---|---|
| Annealed | — | — | — | 285 max |
| Hardened & tempered | 1544 min | 1312 min | 10 min | — |
Hardness values: see our hardness conversion table to convert between HRC, HB, HV and tensile strength.
As Rolled or Annealed.
EN30B is normally supplied either as rolled or annealed. Both describe the state the bar arrives in before you machine it, and the difference shows up at the spindle rather than on the certificate.
Bar in the condition it left the hot rolling mill, with no softening treatment afterwards. Its hardness is whatever the rolling and the cooling that followed happened to leave behind, so it can sit higher — and vary more from bar to bar — than annealed material.
The bar is reheated, held at temperature, then cooled slowly — usually in the furnace itself. That slow cool lets the structure soften and even out, giving lower and more consistent hardness while relieving the stresses rolling left in the bar. It is the softest, most machinable condition this grade comes in, which is where the 285 HB maximum quoted above applies.
For a grade like this the distinction matters twice over. First, all the machining happens before any hardening — annealed bar cuts more easily and is kinder to tooling. Second, a bar with rolling stresses still in it is more likely to move as metal comes off, which shows up as parts drifting out of tolerance on long or asymmetric components. If you are taking heavy cuts or holding tight tolerances, specify annealed on the order rather than assuming it, and check the condition stated on your EN 10204 certificate. Either way, the real hardening happens after machining — harden and temper.
Typical Applications.
- Plastic injection, compression and transfer moulds
- Die-casting dies
- Highly stressed transmission gears and pinions
- Aero-engine connecting rods and differential shafts
- High-load drive shafts and heavy-duty spindles
- Breech mechanisms and small arms components
- Down-hole drilling tools and high-duty bolts
Key Benefits.
- Tensile strength over 1544 N/mm² after hardening and tempering
- Air hardening — minimal distortion and cracking risk
- Hardens right through large sections without a drastic quench
- High fatigue resistance and shock-loading capacity
- Available annealed to 285 HB max where machinability matters
- Available cut to length from one piece — no minimum order
Remarks & Guidance.
Supplied as rolled or annealed — machine first, then harden and temper. Harden from 810–830°C and cool in air; heavy sections may require an oil quench. Temper low — typically not above 250°C where maximum hardness is wanted for tooling and moulds, higher where more ductility is needed. Note this is a through-hardening grade, unlike the case-hardening EN39B (835M15) it shares a nickel level with. Where the full 4% nickel specification is not required, EN24 (817M40) is the more economical high-tensile choice. Welding is not recommended.
Relevant Heat Treatment Processes.
This grade responds to the following heat treatment processes. Click any card for temperatures, cooling methods and expected hardness values.