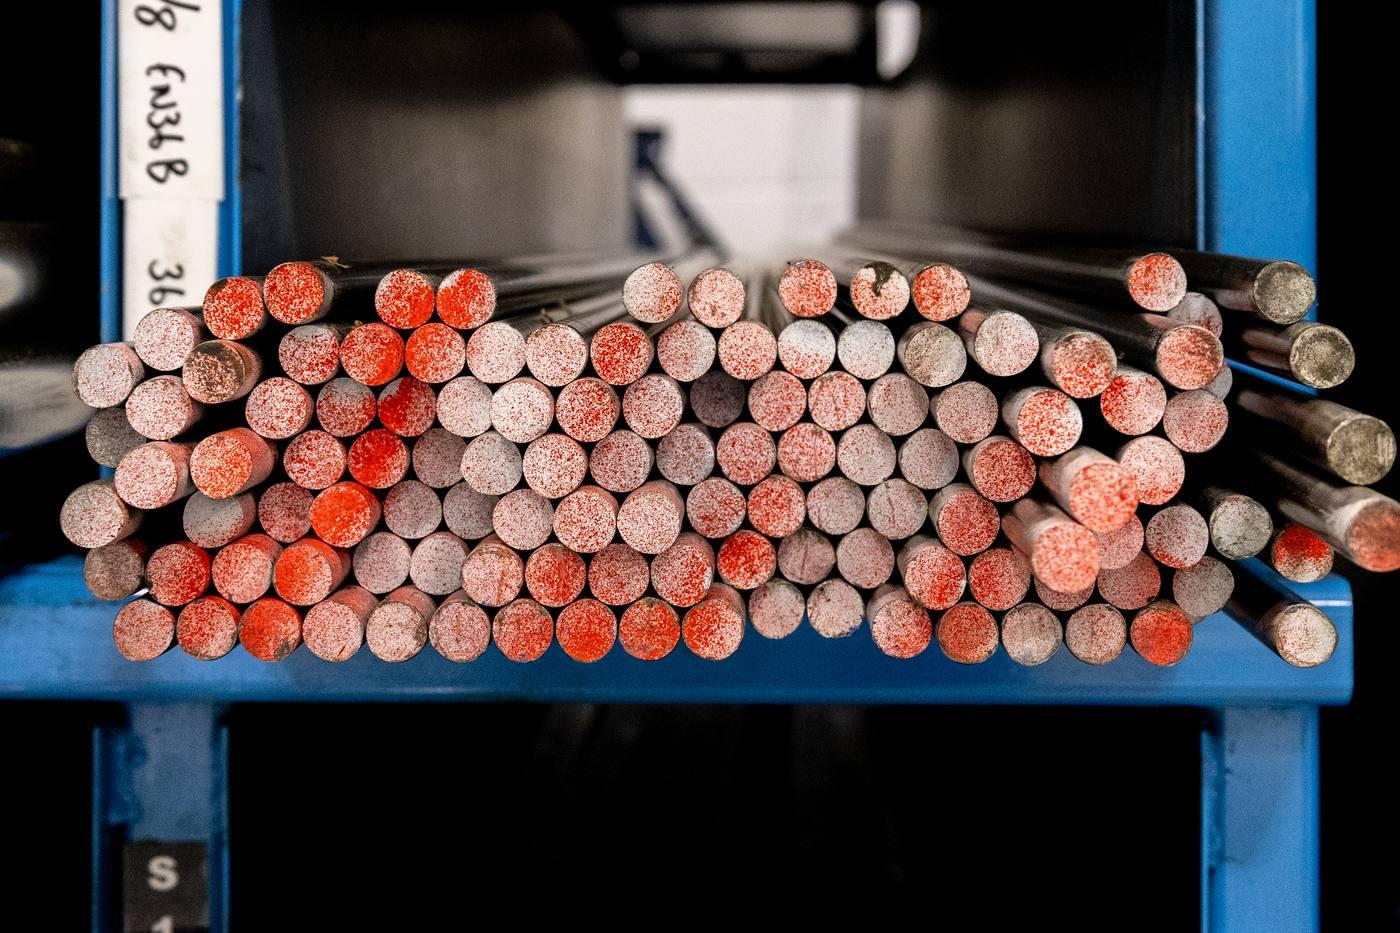
Grade Designations.
| BS EN 10083-3:2006 | 34CrMo4 / 1.7220 |
| BS 970:1991 (withdrawn) | 605M36 |
| AISI/SAE | 4135 |
| DIN | 34CrMo4 / 1.7220 |
| ISO | 34CrMo4 |
Availability & Supply Condition.
Bright Rounds: 8–100mm | Black Rounds: 25–150mm
Supply condition: EN16 is typically supplied in the T condition — hardened and tempered (H&T) — as bright drawn or hot rolled black. It can also be offered as rolled on request, where the bar is to be machined heavily or heat treated after machining. Specify the condition on the order.
Cut to length from 1 piece — −0/+2mm standard tolerance — 2–3 day turnaround — Cutting service details ›
T Condition or As Rolled.
EN16 is a through-hardening grade, so the condition the bar arrives in decides both how it machines and what properties the finished part has.
Hardened and tempered at the mill, so the bar arrives at its working strength with no heat treatment to schedule and no distortion to design around. This is what we normally supply, in both bright drawn and hot rolled black. The tensile figures in the table below are for this condition and vary with ruling section.
Bar in the state it left the hot mill, with no treatment afterwards. The right choice when the part needs heavy machining before it is hardened, or when you intend to harden and temper it yourself after machining. Available on request rather than from stock, so allow lead time.
Specify the condition on the order — it is not implied by the grade name. A bar already in T condition will not machine as freely as as-rolled material, and a part that is to be hardened after machining should not start in T condition. The condition supplied is recorded on the EN 10204 certificate, so it can be checked on arrival. More on our material certification ›
Chemical Analysis.
Values shown as percentages by weight (% wt). Values are ranges unless stated as maxima.
| Designation | C | Si | Mn | P max | S max | Cr | Mo |
|---|---|---|---|---|---|---|---|
| 605M36 | 0.30–0.40 | 0.10–0.35 | 0.70–1.00 | 0.04 | 0.04 | 0.90–1.20 | 0.25–0.35 |
| 34CrMo4 | 0.30–0.37 | 0.17–0.37 | 0.60–0.90 | 0.035 | 0.035 | 0.90–1.20 | 0.15–0.30 |
For full chemical analysis with heat number, request an EN 10204 3.1 material test certificate when ordering — available on all alloy grades. Certificate types explained ›
Mechanical Properties.
Values shown for standard supply condition. Properties vary by section size and heat treatment condition.
| Condition | Size (mm) | Tensile Rm (N/mm²) | Yield Re (N/mm²) | A% min |
|---|---|---|---|---|
| H&T (T) | ≤16 / >16–40 / >40–63 | 900–1100 / 800–950 / 700–850 | ≥700 / ≥600 / ≥500 | 12 / 13 / 14 |
Hardness values: see our hardness conversion table to convert between HRC, HB, HV and tensile strength.
Typical Applications.
- Feedstock for bright bar cold drawing
- Engineering shafts and spindles (medium duty)
- Axles and transmission components
- High-tensile bolting and studs
- Oil and gas downhole components
Key Benefits.
- Better hardenability than plain carbon EN8
- Good response to heat treatment in larger sections
- Lower cost than EN19 for medium-duty applications
- Good machinability in annealed or normalised condition
Remarks & Guidance.
Preheat to 200–300°C before welding. Post-weld heat treatment recommended. For hardening and tempering: oil quench from 850–880°C and temper at 550–660°C. For normalising: heat to 850–870°C and air cool.
Relevant Heat Treatment Processes.
This grade responds to the following heat treatment processes. Click any card for temperatures, cooling methods and expected hardness values.
Normalising refines grain structure and relieves stress after forging or machining.
This grade responds to quench hardening — oil or water quench from austenitising temperature.
Temper after hardening to achieve the required tensile range and reduce brittleness.